3C Electronic Connector Precision Measurement Solution
Posted2026-7-8

High-Speed Stamping Connector Dimensional Consistency Control Solution
3C Electronic Connector Precision Measurement: From Efficiency Bottlenecks to Data-Driven Quality Control
The 3C electronic connector industry faces a structural contradiction: the tension between miniaturization trends and inspection efficiency requirements is widening. When connector pin pitch shrinks below 0.4mm and batch order volumes reach millions, traditional sampling inspection can no longer simultaneously meet the dual pressures of dimensional consistency and production delivery. This is not an equipment precision issue; it requires a redesign of the inspection paradigm.
Detection complexity introduced by miniaturization
Typical characteristics of 3C electronic connectors include miniaturized dimensions, high-density arrangements, and strict tolerance requirements. For example, a motherboard connector in a smartphone may contain dozens of pins, with coplanarity, pitch, and width tolerances all controlled within ±0.02mm. When production cycle times require hundreds of units per minute, manual one-by-one inspection becomes a bottleneck for the entire production line.
The critical issue is that connector reliability depends heavily on dimensional consistency. A minor pin misalignment can scrap an entire motherboard, yet such defects are often missed by functional testing before shipment. Therefore, inspection must be fast enough to detect statistical anomalies and trigger early warnings before batch failures occur.
Dual-View Fusion: Balancing Accuracy and Efficiency
Traditional vision measurement systems face a trade-off: high magnification delivers sub-micron precision but offers a limited field of view, while low magnification provides a wider coverage area but lacks the resolution to capture fine details. Dual-field fusion technology overcomes this by coordinating optical systems to simultaneously acquire both high- and low-magnification images in a single setup, combining the advantages of both fields of view.
This design's practical value lies in its ability to capture both the overall profile (low magnification) and individual pin details (high magnification) simultaneously when measuring a connector, eliminating the need to switch between magnifications. For complex connectors with dozens of measurement features, all data can be collected in a single scan, reducing measurement time from several minutes to just tens of seconds.
Batch testing in flight measurement mode
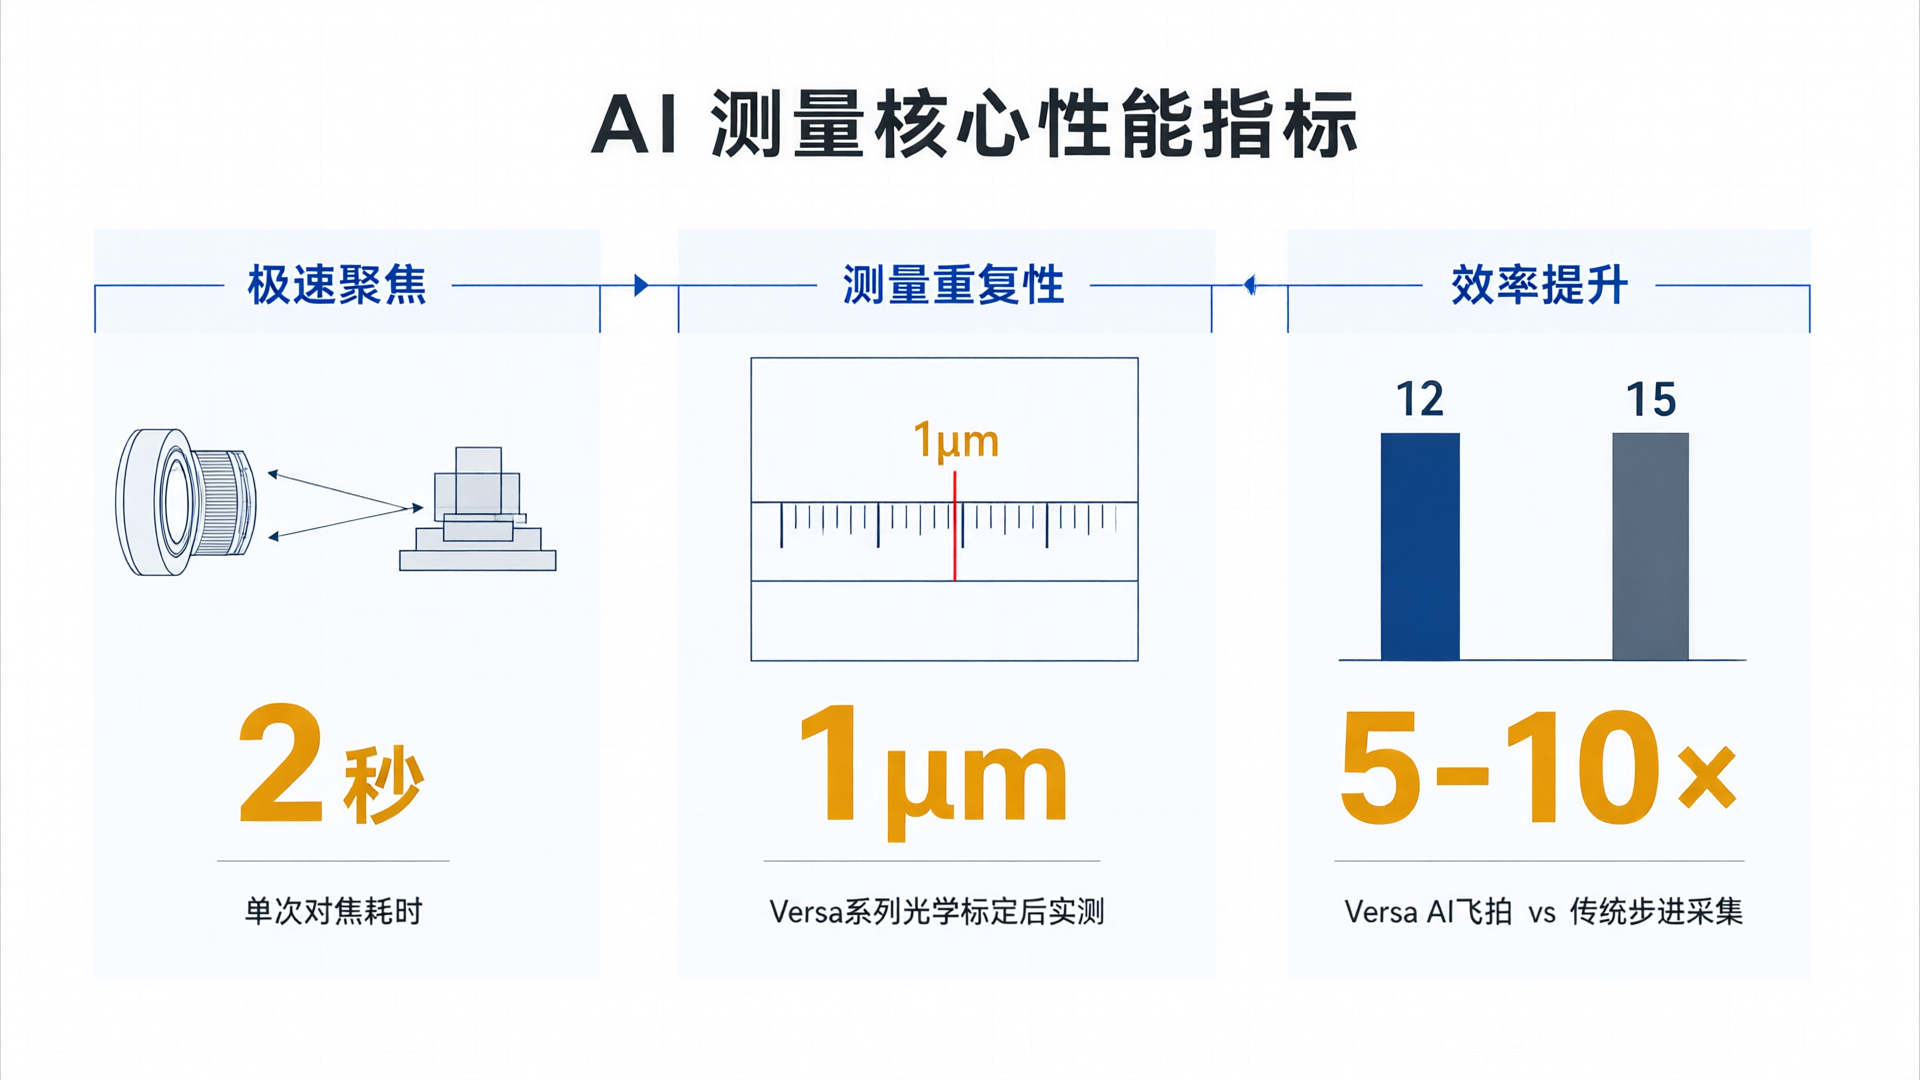
After improving the efficiency of single-piece measurement, the bottleneck in batch inspection shifts to loading/unloading and positioning. The flying measurement mode eliminates the traditional "move-stop-measure-move" cycle through real-time sampling during continuous motion. Samples move continuously on the carrier while the measurement system captures images and identifies features on the fly.
This mode imposes stringent requirements on the control system: image acquisition frequency, motion speed, and image processing algorithms must be precisely synchronized. Any delay in a single component can either result in lost measurement data or motion blur that degrades accuracy. Mature flight-based measurement systems can boost batch inspection efficiency by 3–5 times while maintaining ±0.003mm accuracy.
From Measurement Data to Process Control
Measurement itself isn't the goal; value comes from data-driven process control. Automated SPC (Statistical Process Control) analysis feeds each measurement result in real time to control charts. When a feature dimension consistently deviates from the target or shows abnormal variation, the system automatically triggers an alert. This enables quality managers to adjust process parameters before defects occur at scale—shifting from post-production inspection to proactive prevention.
The online real-time feedback mechanism further shortens the response cycle. Measurement results are pushed directly to the production line control system; when an out-of-spec trend is detected, equipment automatically stops or adjusts processing parameters to prevent defective parts from proceeding to the next step. This closed-loop control compresses the quality issue detection-to-response cycle from hours to minutes.
Deep integration with manufacturing systems
The digital maturity of a modern factory determines the upper limit of value for inspection data. MES (Manufacturing Execution System) integration transforms measurement data from isolated quality records into a fully traceable data chain linked to specific batches, machines, and process parameters. When a customer complaint arises, quality engineers can retrieve all measurement data for the affected batch within minutes to pinpoint the root cause.
This integration also supports advanced data analytics. By correlating measurement data with process parameters, engineers can identify key factors affecting dimensional stability and continuously optimize the manufacturing process. Once sufficient data is accumulated, predictive models can be built to anticipate the impact of equipment wear on product quality in advance.
Practical considerations for implementation
The feasibility of a technical solution ultimately depends on balancing implementation costs with returns. While dual-field-of-view fusion and flight measurement modes require higher equipment investment than traditional vision measurement systems, the labor savings from improved inspection efficiency and defect prevention typically offset the initial investment within 6 to 12 months for 3C connector manufacturers producing at a million-unit monthly volume.
When selecting a detection solution, enterprises must evaluate not only equipment specifications but also the software system's scalability, compatibility with existing production lines, and the vendor's technical support capabilities. A mature precision measurement solution should evolve alongside business growth rather than facing pressure for premature upgrades after capacity ramp-up.
For 3C electronic connector manufacturers planning to upgrade their inspection capabilities, Maike Zhice recommends starting with bottlenecks in actual production lines. First, implement data collection and closed-loop control for critical processes, then gradually expand to a full-process quality management system. The core criterion for technology selection is not the sophistication of parameters, but whether the solution can consistently support the enterprise's capacity goals and quality requirements over 3-5 years.